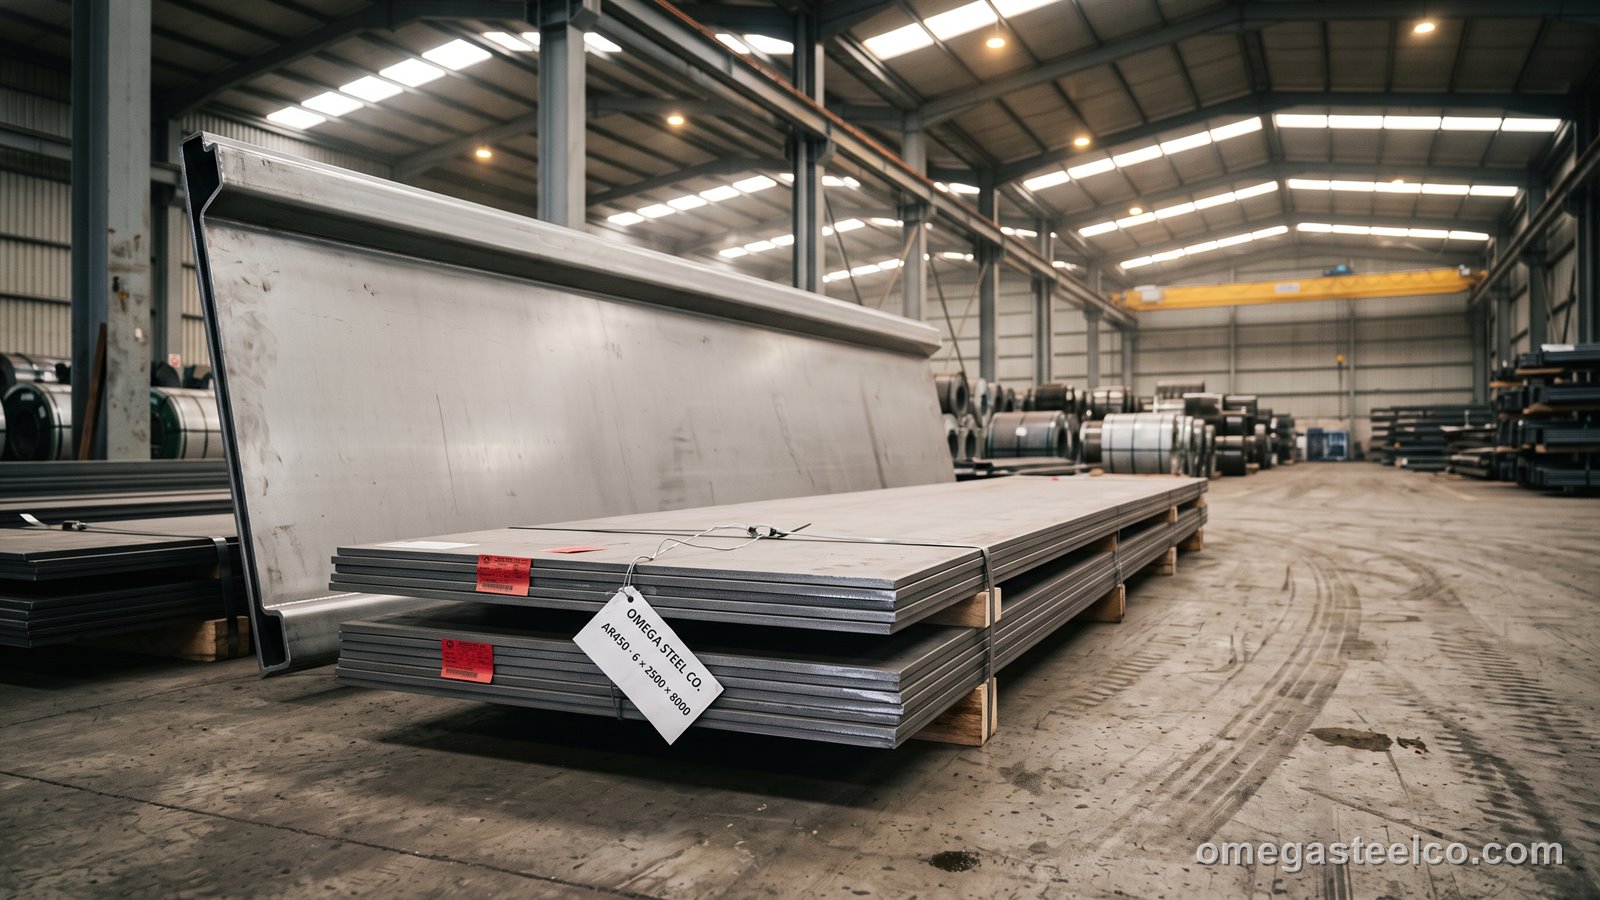
What is AR450 wear plate?
AR450 is a quenched martensitic plate hardened to a nominal 450 HB — the mills guarantee 420–475 — from a chemistry only slightly richer in carbon and boron than AR400. The extra 50 Brinell points buy about 15 % more life in sliding abrasion and a noticeably higher resistance to gouging by sharp rock, while the plate keeps roughly the toughness of AR400 (typically 30–40 J at −40 °C) and can still be cold-bent at 3.5–4 × t. That combination is why it displaced AR400 in the body-building trade in the 2010s: tipper floors went from 8 mm AR400 to 5–6 mm AR450, trailer sides to 4 mm, and the same happened in loader buckets, screens and recycling equipment. The plate is made by every Q&T mill — Hardox 450 is the best-known, with Dillidur 450 V, XAR 450, Raex 450, JFE-EH450 and NM450 as equivalents — and thinner gauges (4–5 mm) are increasingly available as cut sheet and coil from SSAB and thyssenkrupp. Like all AR plate it has no standardised yield strength and loses hardness above about 250 °C, so it is a wear part, not a structural member, and must not be hot-worked or flame-straightened.
Chemical composition
| Element | C | Si | Mn | P | S | Cr | Ni | Mo | B |
|---|---|---|---|---|---|---|---|---|---|
| max. % (ladle) | ≤ 0.26 | ≤ 0.70 | ≤ 1.60 | ≤ 0.025 | ≤ 0.010 | ≤ 1.40 | ≤ 0.25 | ≤ 0.60 | ≤ 0.005 |
CEV about 0.40–0.50 depending on thickness; the higher carbon is what raises the hardness over AR400.
Hardness and mechanical properties
| Property | Requirement | Typical value | Note |
|---|---|---|---|
| Brinell hardness | 420–475 HB | 450 HB | EN ISO 6506-1 |
| Yield strength Rp0.2 | not guaranteed | ≈ 1 200 MPa | |
| Tensile strength Rm | not guaranteed | ≈ 1 400 MPa | |
| Elongation A5 | — | ≈ 10 % | |
| Charpy V | — | ≈ 35 J at −40 °C | longitudinal |
| Max. service temperature | — | 250 °C |
Equivalent grades
| System | Grade | Note |
|---|---|---|
| SSAB | Hardox 450 | reference brand |
| Dillinger | Dillidur 450 V | |
| thyssenkrupp | XAR 450 | |
| SSAB Raahe | Raex 450 | |
| JFE | JFE-EH450 | |
| GB/T 24186 | NM450 | Chinese mills |
Thickness choice for truck bodies and buckets
| Application | AR450 | Replaces | Weight saving |
|---|---|---|---|
| Tipper body floor, aggregates | 5–6 mm | 8 mm AR400 / 10 mm S355 | ≈ 30–45 % |
| Tipper body sides | 4–5 mm | 6 mm AR400 | ≈ 20–30 % |
| Demolition / rock body floor | 8–10 mm | 12 mm AR400 | ≈ 20 % |
| Loader bucket bottom | 12–20 mm | 15–25 mm AR400 | ≈ 15 % |
| Bucket side cutters, wear strips | 20–30 mm | AR400 same | — (longer life) |
| Chute / hopper liners | 6–12 mm | 10–15 mm AR400 | ≈ 25 % |
Savings assume equal wear life in sliding abrasion; with heavy impact keep the thicker AR400 or add wear strips.
Thickness range and stock sizes
| Thickness | Widths × lengths | Availability |
|---|---|---|
| 5–8 mm | 2 000 / 2 500 × 6 000 / 8 000 / 12 000 | stock brands |
| 10–20 mm | 2 000 / 2 500 × 6 000 | stock and mill |
| 25–30 mm | 2 000 / 2 500 × 6 000 | mill order |
| Cut parts | plasma / laser (≤ 25 mm) per DXF | from 500 kg |
Weight per m² and per plate
| Thickness | kg/m² | 1 500 × 6 000 (kg) | 2 000 × 6 000 (kg) | 2 500 × 12 000 (kg) |
|---|---|---|---|---|
| 5 mm | 39.3 | 353 | 471 | 1 178 |
| 6 mm | 47.1 | 424 | 565 | 1 413 |
| 8 mm | 62.8 | 565 | 754 | 1 884 |
| 10 mm | 78.5 | 707 | 942 | 2 355 |
| 12 mm | 94.2 | 848 | 1 130 | 2 826 |
| 15 mm | 117.8 | 1 060 | 1 413 | 3 533 |
| 20 mm | 157.0 | 1 413 | 1 884 | 4 710 |
| 25 mm | 196.3 | 1 766 | 2 355 | 5 888 |
| 30 mm | 235.5 | 2 120 | 2 826 | 7 065 |
Nominal weights — mill tolerance to EN 10029 class A adds up to +4 % on thin plate; invoiced on theoretical weight unless agreed otherwise.
Bending, cutting and welding
Cold-bend at ≥ 3.5 × t transverse (4.5 × t longitudinal) with a die width of 12–16 × t and ground edges; large-radius body folds are routine on a 6–8 m press brake. Plasma and laser cut without preheat up to 20 mm; oxy-fuel needs 150 °C preheat above 20 mm. Weld with low-hydrogen processes and soft consumables (≤ 500 MPa yield); preheat from 15 mm (100–125 °C), interpass ≤ 225 °C, and avoid welding across the whole width of a highly stressed floor in one pass. Drill with carbide or cobalt HSS at half the speed used for S355.
Where it is used
- Tipper, dump-truck and trailer bodies (floor and sides)
- Loader and excavator buckets, screens and grizzlies
- Recycling, shredder and crusher wear parts
- Chutes, hoppers, cyclones and conveyor liners
- Agricultural blades, cultivator points and wear plates
- Concrete and asphalt plant liners
AR450 vs AR400 vs AR500
Against AR400, AR450 gives 10–15 % more life for a small bending penalty and about the same price — the reason it has become the default. AR500 is 10–15 % harder again but much less forgiving: it bends at 5 × t, needs preheat for welding and is reserved for flat liners and fixed parts. For load-bearing wear parts use S690QL.
Price
Quoted per plate or per cut part rather than by list band; the offer depends on brand, thickness and quantity and follows the European Q&T plate lists. Send the size list for a firm price within a working day.
Bands from our weekly export list (September 2026), FOB Istanbul, full-container quantities, excluding freight and certificates. Firm price per project on RFQ within one working day.
Export and packing
AR450 wear plate is packed as follows: plates on bearers, banded; cut parts palletised. Loading: 20' ≈ 20 t; 40' HC ≈ 24 t; 8 m plate on flat-rack. The HS heading depends on the product: 7208 / 7209 / 7210 for carbon strip, 7225 / 7226 where alloyed.
| Term | Detail |
|---|---|
| MOQ | 1 plate (cut parts from 500 kg) |
| Incoterms | FOB Istanbul · CIF / CFR Gulf, Africa · DAP EU, Balkans, Iraq, Caucasus · DAP Aktau |
| Lead time | Stock 3–7 working days; mill order 4–6 weeks |
| Packing | Plates on bearers, banded; cut parts palletised |
| Container / truck | 20' ≈ 20 t; 40' HC ≈ 24 t; 8 m plate on flat-rack |
| Documents | Invoice, packing list, EN 10204 3.1 (3.2 on request), certificate of origin; SASO / SONCAP / PVoC on request |
| Payment | 30% advance, balance against B/L copy; L/C at sight for orders above 100 t |
Certificates and testing
The paperwork travelling with AR450 wear plate is an EN 10204 3.1 certificate covering chemistry, mechanical values and the delivery condition. If your specification calls for an inspected release, ask for 3.2 at enquiry stage — it changes the mill slot, not only the paperwork. EN 10160 ultrasonic reports and supplementary impact tests at your design temperature are available on plate above 8 mm.
How to order
Specify AR450 (or brand), thickness × width × length or DXF, quantity, bending plans and certificate; thin gauges (4–5 mm) in coil or cut sheet on request.
Standards
- Mill specifications (Hardox 450, Dillidur 450 V, XAR 450, Raex 450, NM450)
- EN ISO 6506-1
- EN 10029
- EN 10204 3.1
Grades
Grade data sheets (chemistry, mechanicals, equivalents) are on our reference site: AR450 · AR400 · AR500
Frequently asked questions
What is AR450 plate?
Quenched abrasion-resistant plate with 420–475 HB hardness (nominal 450) — about 15 % more wear life than AR400 with nearly the same formability; the standard grade for tipper bodies and buckets.
Is AR450 the same as Hardox 450?
Hardox 450 is the SSAB brand of AR450-class plate; Dillidur 450, XAR 450, Raex 450 and NM450 are equivalents from other mills.
What bend radius does AR450 need?
About 3.5 × thickness transverse and 4.5 × longitudinal, with ground edges and a die width of 12–16 × t.
Can AR450 be welded without preheat?
Up to about 15 mm yes, with low-hydrogen consumables; thicker plate or combined thickness above 30 mm needs 100–125 °C preheat.
What thickness of AR450 for a tipper floor?
5–6 mm for aggregates and soil, 8–10 mm for rock and demolition — replacing 8–12 mm AR400 with 20–45 % less weight.