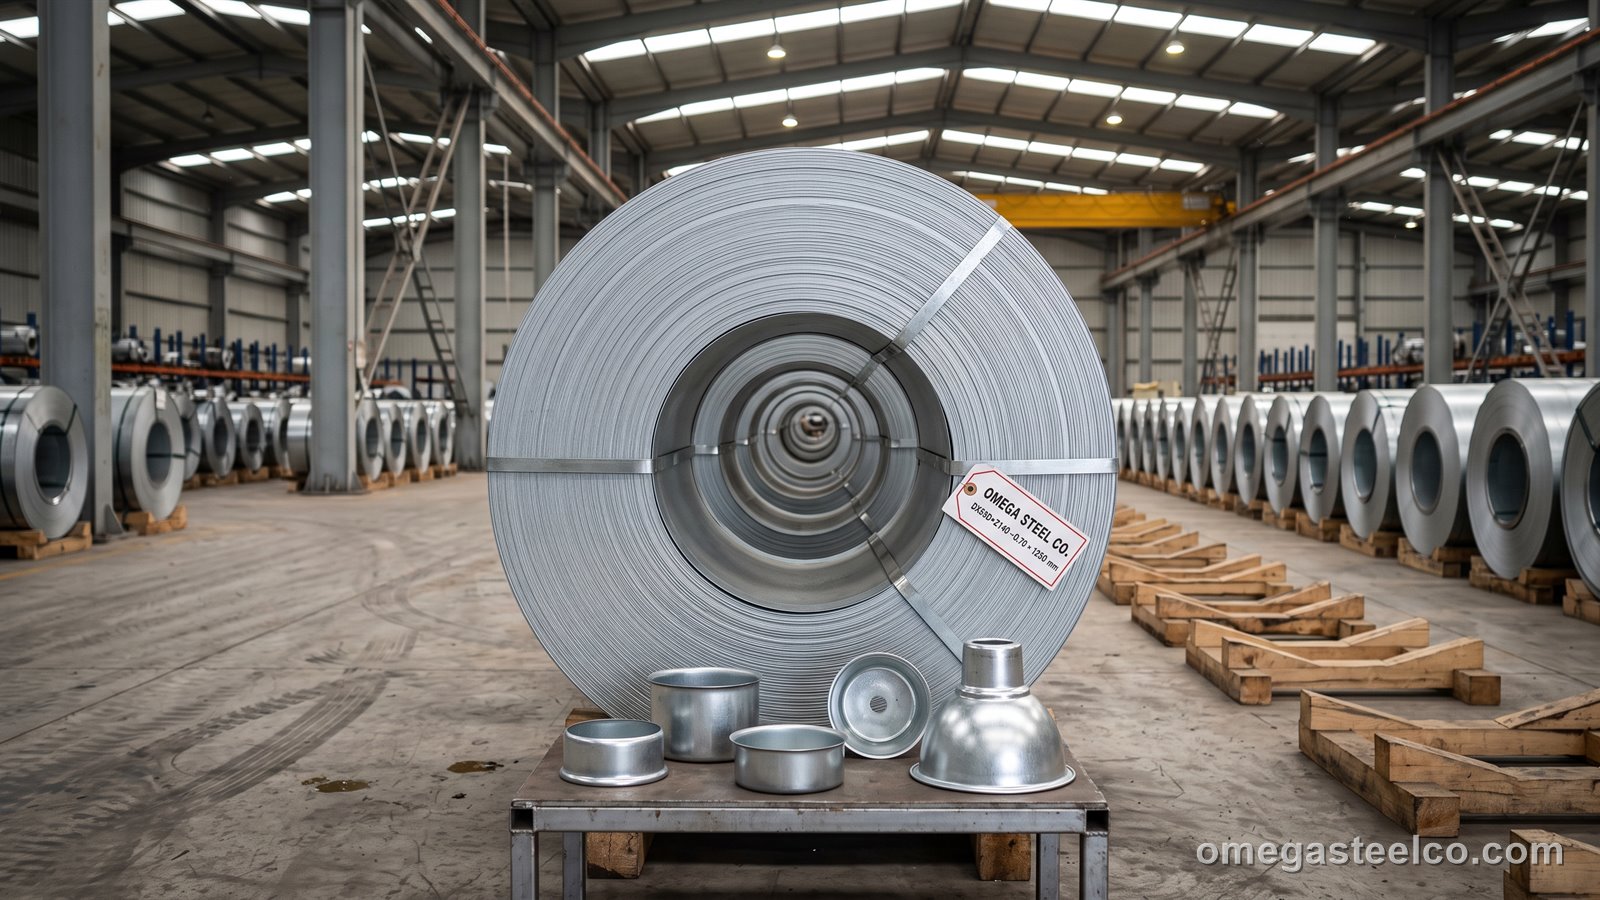
What is DX53D galvanized steel?
DX53D is the third forming level in EN 10346: after DX51D (bending) and DX52D (drawing) comes deep drawing. The substrate is an aluminium-killed, extra-low-carbon cold-rolled steel whose grain and texture are controlled during annealing to give a high plastic strain ratio (r ≈ 1.5–1.8) and a low yield ratio — the steel thins uniformly instead of necking, so it can be drawn to a depth greater than its diameter. The standard guarantees yield 140–260 MPa, tensile 270–380 MPa and 30 % elongation (A80), and mills add a non-ageing guarantee so the sheet does not develop stretcher strains after months in stock. The zinc coating is the same Z100–Z275 family, usually ordered minimised-spangle with surface quality B; the coating itself must survive the draw, which is why coating class and lubricant are specified together with the grade. DX53D covers most deep-drawn galvanized parts; DX54D (r ≥ 1.6, 36 %) and DX56D/57D exist for the extreme automotive cases.
Chemical composition
| Element | C | Si | Mn | P | S | Ti |
|---|---|---|---|---|---|---|
| max. % (ladle) | 0.10 | 0.50 | 0.60 | 0.08 | 0.030 | 0.30 |
Typical heat: C 0.02–0.04, Mn 0.15–0.20, Al 0.03–0.06 (killed).
Mechanical properties and deep-drawing indices
| Property | Requirement | Typical value | Note |
|---|---|---|---|
| Yield strength Rp0.2 | 140–260 MPa | 160–210 MPa | |
| Tensile strength Rm | 270–380 MPa | 290–340 MPa | |
| Elongation A80 | ≥ 30 % | 34–42 % | |
| r90 (plastic strain ratio) | not specified | ≈ 1.6 | DX54D guarantees ≥ 1.6 |
| n90 (hardening exponent) | not specified | ≈ 0.20 | |
| Ageing | non-ageing on agreement | 6 months |
Equivalent grades
| System | Grade | Note |
|---|---|---|
| EN 10142 (old) | DX53D+Z (EN 10142) | withdrawn 2004 |
| DIN 17162 | St 05 Z+Z (EN 10142) | historic German |
| JIS G3302 | SGCD2 | |
| ASTM A653 | DDS Type A / Deep Drawing Steel | coating G90 ≈ Z275 |
| GB/T 2518 | DX53D+Z |
What the coating does in a deep draw
| Class | Zinc mass (g/m², both sides) | Thickness per side (µm) | Typical life C3 | Where used |
|---|---|---|---|---|
| Z100 | 100 | ≈ 7 | 4–6 years | deep-drawn cups, housings and sinks |
| Z140 | 140 | ≈ 10 | 6–9 years | drawn parts with a painted or enamelled finish |
| Z200 | 200 | ≈ 14 | 9–13 years | the upper limit for deep drawing — test the die first |
The coating is drawn with the steel, so the variable that matters is not mass but the thickness of the brittle intermetallic layer between zinc and substrate. Minimised spangle (M) and surface quality B give the most predictable draw and the best paint adhesion; specify chromate-free passivation if the part is powder-coated afterwards.
Thickness range and stock sizes
| Thickness | Widths × lengths | Availability |
|---|---|---|
| 0.40–0.80 mm | coil 1 000 / 1 250 mm; blanks to size | to order 3–4 weeks |
| 1.0–2.0 mm | coil 1 000 / 1 250 / 1 500 mm | to order 3–4 weeks |
Weight per m² and per sheet
| Thickness | kg/m² | 1 000 × 2 000 (kg) | 1 250 × 2 500 (kg) | 1 500 × 3 000 (kg) |
|---|---|---|---|---|
| 0.4 mm | 3.28 | 6.6 | 10.3 | 14.8 |
| 0.5 mm | 4.07 | 8.1 | 12.7 | 18.3 |
| 0.6 mm | 4.85 | 9.7 | 15.2 | 21.8 |
| 0.7 mm | 5.64 | 11.3 | 17.6 | 25.4 |
| 0.8 mm | 6.42 | 12.8 | 20.1 | 28.9 |
| 1 mm | 7.99 | 16.0 | 25.0 | 36.0 |
| 1.2 mm | 9.56 | 19.1 | 29.9 | 43.0 |
| 1.5 mm | 11.92 | 23.8 | 37.2 | 53.6 |
| 2 mm | 15.84 | 31.7 | 49.5 | 71.3 |
Includes Z140 coating; add 0.135 kg/m² for Z275.
Forming, welding and painting
Draw ratios to about 2.0 in one stage; use drawing oil compatible with zinc, polished or coated tools and adequate blank-holder force to avoid wrinkling — the low yield makes the sheet prone to it. The coating stays intact through the draw when Z140–Z200 and minimised spangle are chosen; heavy Z275 on deep parts may flake at sharp radii. Spot welding with pulsed current; MAG with fume extraction. Paint after degreasing; passivation C or a thin organic coating (TOC) on request.
Where it is used
- Deep-drawn housings, cups and cylinders
- Extractor hoods, lamp and luminaire bodies
- Water-heater inner cups and appliance drums
- Automotive and trailer brackets and reinforcements
- Fuel-tank and reservoir shells (non-pressure)
- Complex HVAC and ventilation pressings
DX53D vs DX54D
DX54D tightens the yield window to 120–220 MPa, raises elongation to 36 % and guarantees r90 ≥ 1.6 and n90 ≥ 0.18 — the automotive deep-drawing level for body panels and the deepest cups. DX53D covers everything short of that at a lower price and shorter lead time. If the part has drawn successfully in DX53D-class material before, stay with it; move to DX54D only when a draw ratio above 2 or an r-value requirement is written into the specification. For shallower parts, DX52D is enough.
Price
DX53D is priced about 40 USD/t over DX51D; the band below is indicative FOB Istanbul for mill-order coil in the usual 0.40–2.0 mm range.
Bands from our weekly export list (September 2026), FOB Istanbul, full-container quantities, excluding freight and certificates. Firm price per project on RFQ within one working day.
Export and packing
DX53D for press work is shipped oiled and fully wrapped - VCI paper against the strip, a moisture barrier over it, edge protectors, and slit widths banded separately so the press feed sees no handling damage. Cradle-packed coils are 5-20 t; blanks go on skids under 3 t. HS 7210.49.
| Term | Detail |
|---|---|
| MOQ | One coil (10–20 t) |
| Incoterms | FOB Istanbul · CIF / CFR Gulf, Africa · DAP EU, Balkans, Iraq, Caucasus · DAP Aktau |
| Lead time | To order 3–4 weeks |
| Packing | Coil eye-to-sky on cradle, VCI wrap, paper interleaved sheet on skids |
| Container / truck | 20' one coil ≤ 20 t; 40' HC two coils |
| Documents | Invoice, packing list, EN 10204 3.1 (3.2 on request), certificate of origin; SASO / SONCAP / PVoC on request |
| Payment | 30% advance, balance against B/L copy; L/C at sight for orders above 100 t |
Certificates and testing
Documentation for DX53D covers the mechanical values, the r90 and n90 figures where the mill measures them, and the coating mass. An EN 10204 3.1 certificate is standard; 3.2 with a third-party inspector is arranged on request. For press shops we can add an Erichsen cupping result taken from the same coil.
How to order
Specify thickness × width, coating class and spangle, surface B, treatment (O for pressing), non-ageing requirement, the part drawing if available, and tonnage; mill slot within one working day.
Standards
- EN 10346:2015 — DX53D+Z, 1.0355
- EN 10143 — tolerances
- EN 10204 3.1
- Former EN 10142 / DIN 17162 St 05 Z
Grades
Grade data sheets (chemistry, mechanicals, equivalents) are on our reference site: DX53D · DX52D · DX54D
Frequently asked questions
What is DX53D steel?
The deep-drawing hot-dip galvanized steel of EN 10346 (1.0355): Al-killed extra-low-carbon substrate, yield 140–260 MPa, elongation ≥ 30 %, r-value about 1.6, coating Z100–Z275.
What is the ASTM equivalent of DX53D?
ASTM A653 DDS Type A (Deep Drawing Steel); JIS G3302 SGCD2.
What is the difference between DX53D and DX54D?
DX54D has a narrower yield window (120–220 MPa), 36 % elongation and guaranteed r90 ≥ 1.6 / n90 ≥ 0.18 for automotive-class deep drawing; DX53D is the general deep-drawing grade.
Which zinc coating for deep drawing?
Z140–Z200 with minimised spangle keeps the coating intact in deep draws; Z275 may flake at sharp radii on deep parts.